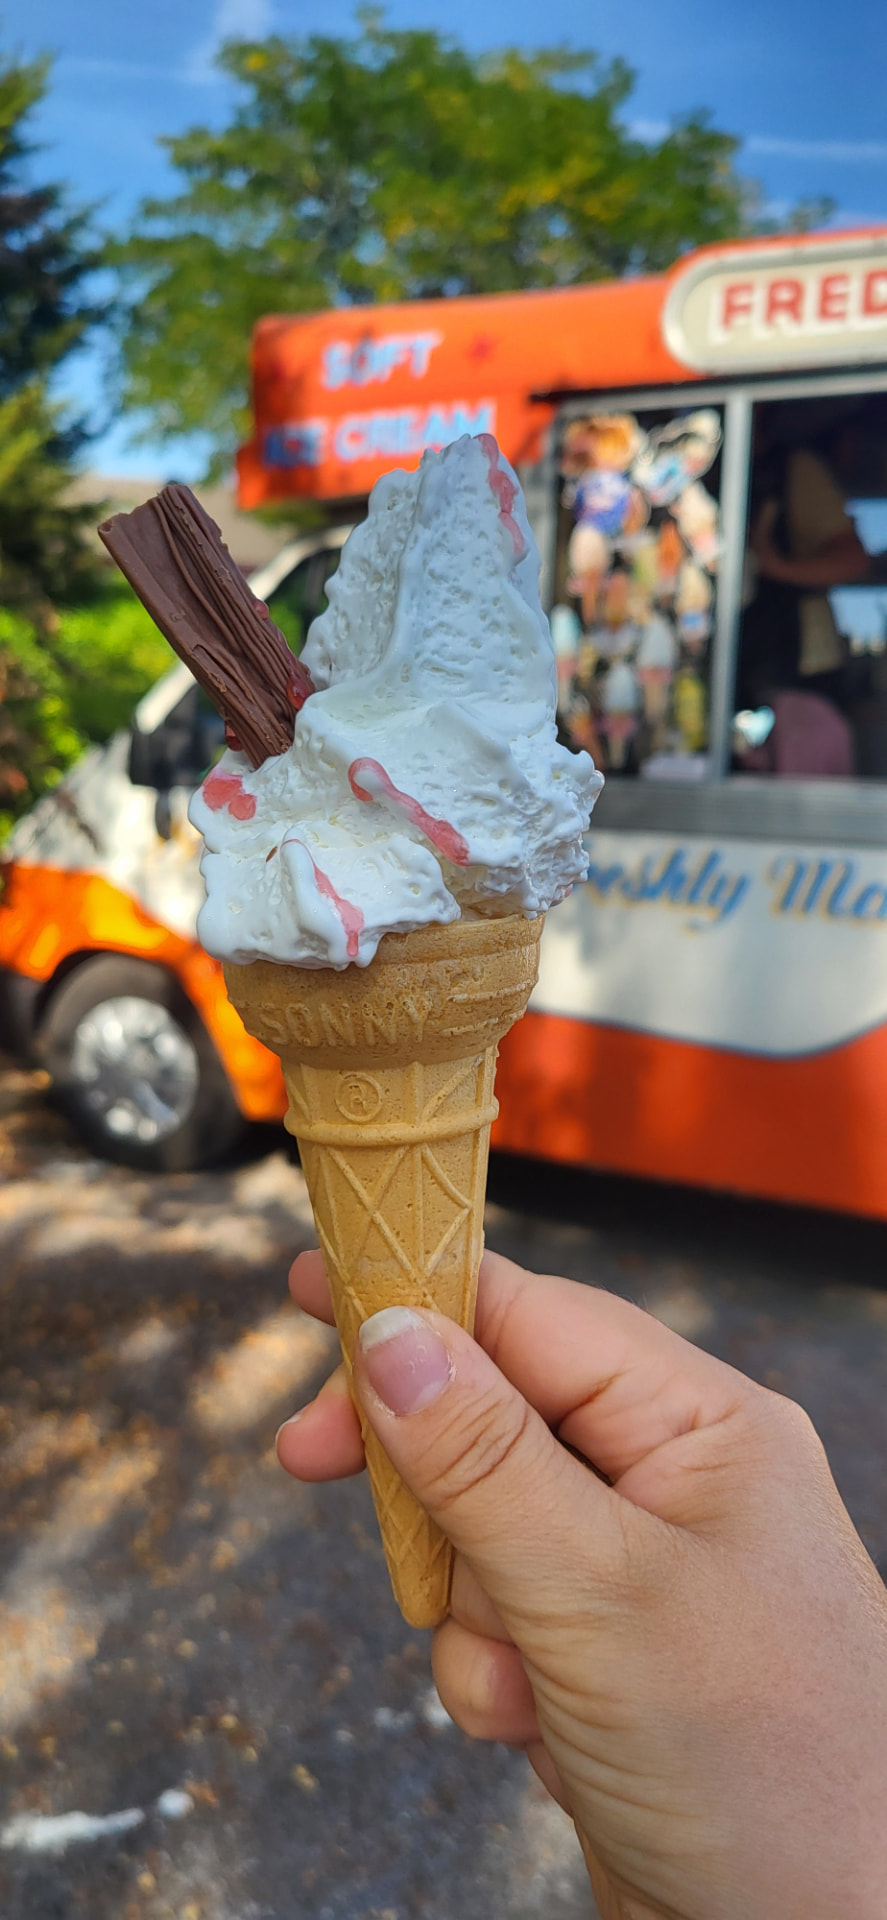
Yesterday afternoon in Northwich, the ice cream van rolled up outside the office. Dylan heard the chimes, and to his enormous credit he did not pretend he had not. He was out of the door at a pace we have not seen from him since the last fire drill.
So Alphabond bought the team ice creams. James, Brook and Andy queued up, the ice cream lady dispensed 99s with about four cones wedged between her fingers at once, which is a skill nobody gives her enough credit for, and for roughly ninety seconds everyone was very happy.
Then the reviews came in.
Brook, who guards the Alphabond expenses like a border collie guards sheep, had two observations. One, the raspberry sauce was on the mean side. Two, and this is the part he really wanted on the record, a 99 costs an awful lot more than 99 pence these days.
The other thing that happened is that the ice cream started melting before anyone had properly got going on it. It hit around 33 degrees yesterday and my phone reckons 34 today. Soft serve does not stand a chance in that.
Which, if you make things and stick them together for a living, is not just a nice bit of office trivia. The same physics that ruins a 99 in a car park is quietly ruining bonds on production lines all over the country this week.
Heat does not weaken hot melt, it slows it down
The instinct is that heat makes adhesive weaker. That is not really what is happening on the line.
Hot melt adhesive works by being applied molten, wetting out the substrate, then cooling and solidifying fast enough to hold the joint once compression is released. The whole system depends on cooling. Take the cooling away and you have not weakened the glue, you have simply not let it do its job yet.
On a 34 degree day, three things change at once:
Your board is hot. Not the air, the board. Corrugated that has been sitting in a warehouse or a trailer in the sun can be a lot hotter than the ambient reading on the wall. Adhesive applied to warm board sheds its heat far more slowly than adhesive applied to board at 18 degrees.
Set time stretches. Your compression section was almost certainly set up for normal conditions. If the adhesive needs longer to cool through and the belt does not, the joint leaves compression before the bond has developed.
Open time stretches too. That sounds like good news, and in isolation it is. Combined with a longer set time it means the adhesive stays fluid and mobile for longer than your line was designed around.
Put those together and you get the classic summer complaint: cases that looked fine at the end of the line, sitting there with their minor flaps yawning open by the time they reach the palletiser.
Why adding more glue usually makes it worse
This is the one worth knowing, because it is the first thing most people try. Pop-opens appear, so someone turns the bead up. It feels logical. More adhesive, stronger bond.
Except a bigger bead has more thermal mass, so it holds its heat longer, so it takes longer to set. You have made the exact problem you were trying to fix slightly worse, and you are now paying more per case for the privilege. Brook would have something to say about that.
If you are getting pop-opens in hot weather, more glue is rarely the answer. Faster setting glue, more compression time, or cooler board usually is.
The other heat problem: the one that happens after the line
Everything above is about the line. There is a second issue that shows up later, and it is the one that generates the awkward phone calls.
A pack can be assembled perfectly, pass every check, go onto the pallet looking immaculate, and then spend eight hours in a trailer where the internal temperature climbs well past anything your factory ever sees. Sunlit trailers and containers get genuinely brutal. If the adhesive's heat resistance is below that, the bond softens, the load shifts, and the pallet that left you in perfect order arrives looking like it has been through something.
That is not a line problem and no amount of adjusting your compression section will fix it. That is a question of whether the grade you are running has the heat resistance your supply chain actually demands, which is a different conversation and one worth having before August rather than after it.
What we would actually check this week
- Measure the board, not the room. An infrared thermometer pointed at the board just before the applicator will tell you more in ten seconds than a week of guessing. If it is materially warmer than usual, you have found your variable.
- Time your compression, honestly. Not what the manual says. What the line is actually giving the joint at today's speed.
- Check where the board has been stored. Board that has been baking in a hot, dry warehouse is both warmer and stiffer, and stiffer flaps push back harder against a joint that has not set yet.
- Resist the urge to turn the tank up. Running hotter to help it flow gives the adhesive even more heat to lose, and sustained overheating degrades the adhesive and chars your tank. Two problems, no benefit.
- Resist the urge to turn the bead up. See above.
- Look at where the finished pallets go. If the failures are appearing downstream rather than on the line, the answer is heat resistance, not line settings.
- Ask whether the grade is right for the season. Some operations genuinely benefit from a different grade in high summer. Some do not. It is worth knowing which you are.
And the honest answer
Sometimes the fix is a different adhesive. Often it is not. Plenty of summer pop-opens turn out to be a compression setting, a storage habit, or board arriving at a temperature nobody had thought to measure. We would rather tell you that and keep you running than sell you a pallet of something you did not need.
If your cases are popping open this week and you would like a second opinion from someone who has seen it a few hundred times, give us a ring on 0845 521 2057 or book a slot and we will talk it through. No charge, no obligation, and if the answer is adjust your belt then that is what we will tell you.
Just try to make sure your factory is not so hot that your 99 melts before you get to the flake.